

High-Throughput Contaminant Detection for Unpackaged, Free-Flowing Materials
The MPI X-Ray Inspection System for Bulk Products is engineered for continuous, noninvasive inspection of loose, unpackaged materials moving on a conveyor belt, such as powders, granules, flakes, or particulate products. Designed for upstream and midstream applications in food, pet food, chemical, and pharmaceutical processing, this system delivers high-sensitivity foreign material detection without disrupting product flow.
Leveraging advanced dual-energy X-ray technology, the system detects various contaminants, including metal, glass, bone, rubber, and dense plastic—even in small fragments—before the product is packaged. It is ideal for early-stage inspection, where rejecting contaminants minimizes product waste and maximizes operational efficiency.
Built for sanitary washdown environments and customizable for line width, product depth, and reject method. MPI’s bulk X-ray system is critical in preventing downstream contamination, safeguarding equipment, and ensuring final product safety and compliance.


Benefits of the Bulk Product X-Ray Inspector From Magnetic Products, Inc
Comprehensive Foreign Object Detection
It detects ferrous and non-ferrous metals, stainless steel, bone, stone, ceramic, glass, rubber, and dense plastics, even in fine or dusty product streams, providing a wider detection range than traditional metal detectors.
Designed for Unpackaged Product Streams
It is optimized for loose-flowing materials such as grains, powders, granules, and chopped or shredded food items on conveyor belts. It is perfect for pre-packaging and ingredient inspection points.
Advanced Dual-Energy Imaging
Differentiate materials based on atomic density, enabling the reliable detection of low-density contaminants often missed in bulk product environments.
High-Throughput Operation
Capable of inspecting bulk material flows at high line speeds (up to 100 meters per minute), ensuring minimal bottlenecks in production lines with continuous product flow.
Precision Reject Mechanism Integration
It is compatible with high-speed reject systems such as multi-flap air nozzles, segmented reject belts, or mechanical diverters that remove only contaminated portions of the product stream, reducing waste and maximizing yield.
Sanitary, Washdown-Ready Construction
Stainless steel frame and conveyor with sloped surfaces and IP65+ or IP69K enclosures. Built to meet USDA, FDA, and 3-A hygiene requirements in wet or dusty processing environments.
Real-Time Inspection with Automated Data Logging
Continuously inspects product flow while logging inspection results, time stamps, rejection events, and image captures, ideal for audits, traceability, and regulatory compliance.
Customizable for Product Depth and Line Width
Available in various aperture heights and conveyor widths to accommodate shallow layers or deeper product beds, depending on bulk density and application.
Bulk Product X-Ray Inspector Product Details
How It Works
MPI’s X-Ray Inspection System for Bulk Products uses a top-down X-ray beam combined with a high-resolution line-scan detector to inspect free-flowing materials conveyed in a continuous stream. The system uses material density contrast to identify foreign objects.
Product Presentation
Unpackaged material is fed onto a conveyor belt in a continuous layer. A product spreader or leveling system may be used upstream to ensure consistent depth and coverage across the belt.
X-Ray Imaging
A low-dose X-ray beam is emitted above and penetrates the entire product layer. The dual-energy detector below captures the X-ray image in real time, measuring differences in material absorption.
Contaminant Identification
The system’s intelligent image processing software analyzes the scanned image for:
Density anomalies (foreign objects)
Size, shape, and contrast variations
Location within the product stream
Contaminant Location & Ejection
When a contaminant is identified:
The system pinpoints its location on the belt using timing and position data.
A precise reject mechanism (such as air nozzles or pushers) removes the contaminated portion from the stream, without halting flow.
Data Capture & Quality Assurance
Every event is logged with images, timestamps, product ID, and rejection cause. Optional integration with plant networks allows real-time monitoring and compliance reporting.
Bulk Product X-Ray Inspector Specification Table
US Customary Units
Compatibility Check - Bulk Product X-Ray Inspector Installations
We operate under the philosophy of The Game of Work.
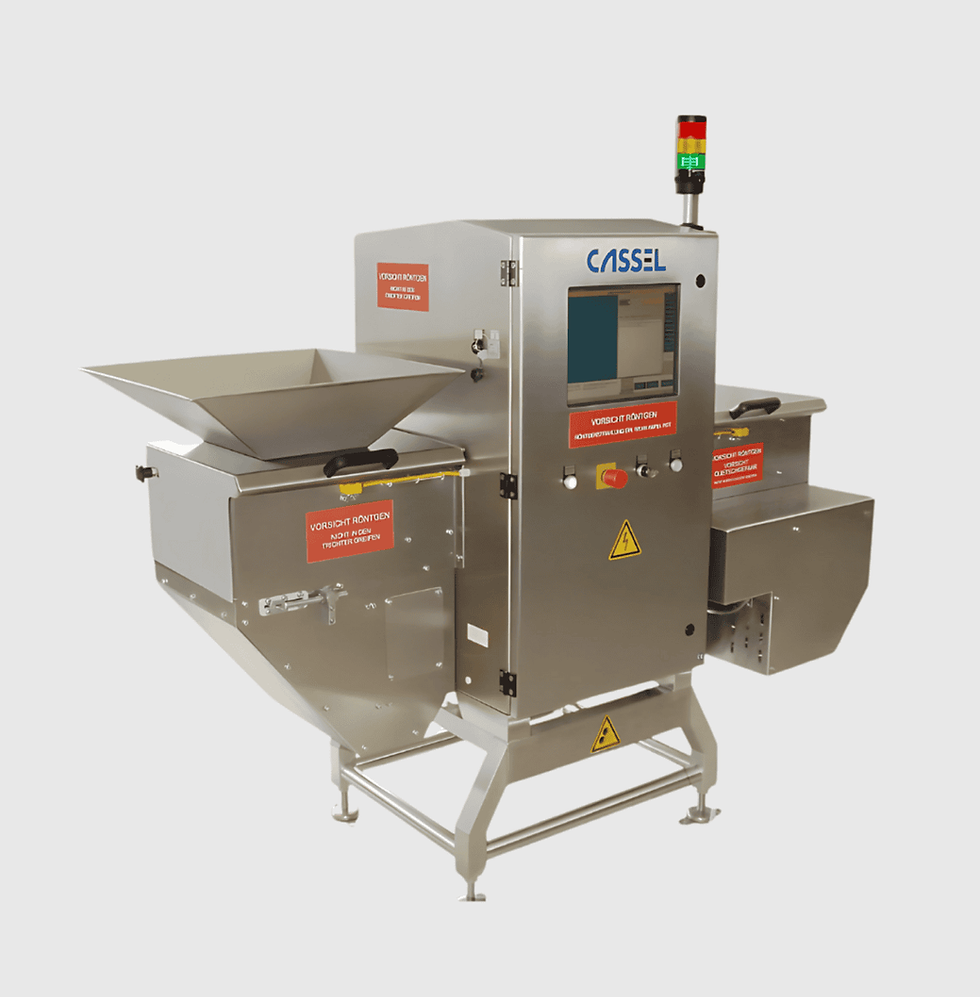
Bulk Flow X-Ray Used in Nut and Almond Processing

Bulk X-ray with XIA Image Processing Software for Dried Fruit and Legume Application

Bulk X-ray with Integrated Reject Flap for Confections and Candy Manufacturing